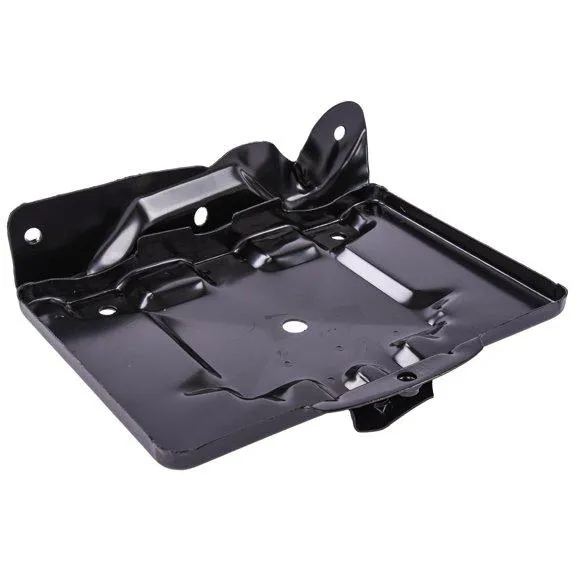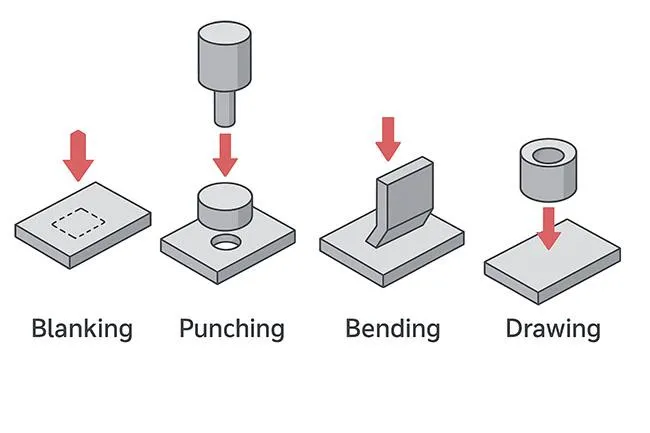
Metal forming is the process of changing the shape of a metal sheet through controlled deformation. In automotive manufacturing, this principle allows flat sheets of steel or aluminum to be transformed into three-dimensional panels, structural reinforcements, brackets, supports, and other components.
The metal forming principle is based on the relationship between material properties, applied force, tool geometry, and material flow. When a sheet is placed between the working surfaces of a forming die, the press generates force and the die transfers that force to the material. If the applied stress exceeds the material’s elastic limit, the sheet undergoes permanent plastic deformation and retains the new shape after the forming operation.
Unlike a process that simply removes material, forming aims to redistribute and deform the existing material to achieve the required geometry.
Understanding this principle is particularly important when developing automotive stamping dies because part geometry, material strength, thickness, forming depth, tool radius, and material flow all influence the final result.
What Is the Basic Principle of Metal Forming?
The basic metal forming principle can be understood through four elements:
Material + Force + Tool Geometry + Controlled Deformation
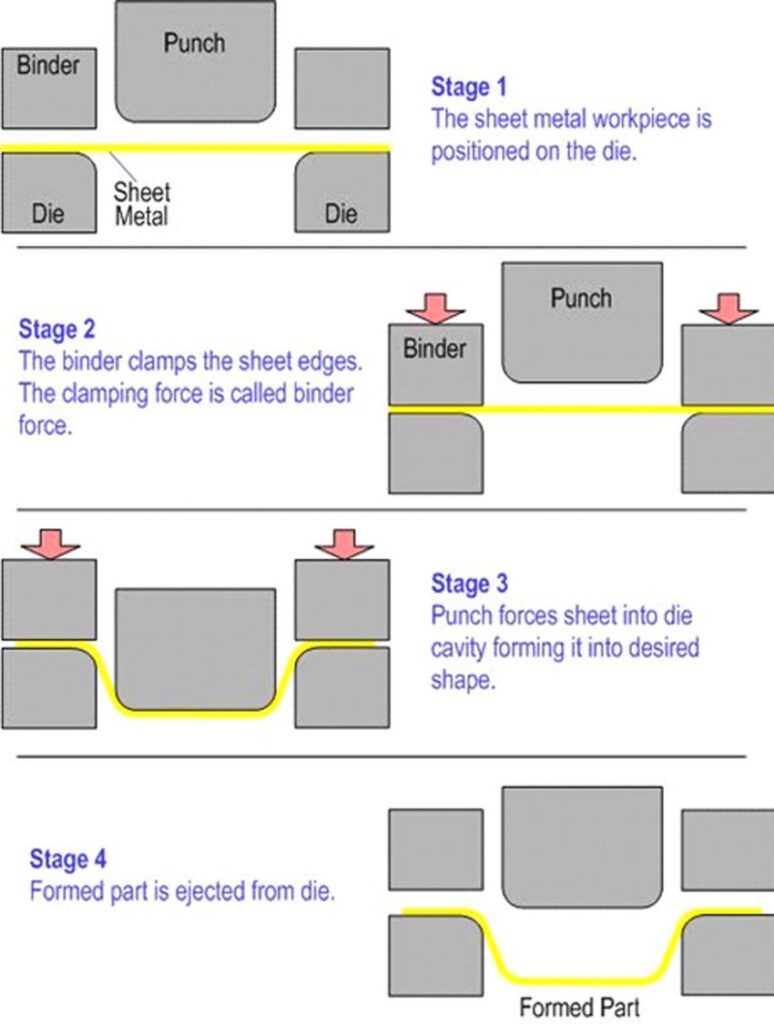
A flat metal sheet initially has a relatively simple geometry. During forming, the press applies force through the die and punch. The sheet responds to this force by stretching, compressing, bending, or flowing into the available forming space.
When the loading conditions are properly controlled, the material reaches the desired shape without excessive cracking, wrinkling, or distortion.
The forming process can therefore be viewed as a controlled transfer of mechanical force into permanent material deformation.
How Does Sheet Metal Deform During Forming?
Sheet metal does not move randomly when a forming die closes. Its deformation is controlled by the interaction between the material and the tooling.
Several deformation behaviors can occur simultaneously.
Bending Deformation
Bending occurs when the sheet is forced around a radius.
The material on one side of the sheet is mainly compressed while the opposite side is mainly stretched. The bending radius of the forming tool has an important influence on the amount of deformation.
A suitable radius helps distribute the forming strain and reduces the risk of cracking.
Stretching Deformation
Stretch forming occurs when the material is pulled over a forming surface.
The sheet becomes thinner in areas experiencing significant tensile strain. If the local strain becomes too high, cracks may develop.
This is especially important for automotive components with large curved surfaces or significant geometric transitions.
Compression
Compression occurs when material is pushed together during forming.
Excessive compression can create instability in the sheet and may contribute to wrinkles. Therefore, the forming process must maintain an appropriate balance between tensile and compressive forces.
Material Flow
Material flow is one of the most important concepts in automotive metal forming.
Instead of treating the sheet as a rigid object, engineers need to understand how material moves from one area of the blank into another during forming.
The amount and direction of material flow can influence:
- Wall thickness
- Surface quality
- Dimensional accuracy
- Wrinkling
- Cracking
- Springback
- Final part geometry
A well-designed forming die controls this material movement rather than simply forcing the entire blank into a shape.
The Role of the Forming Die
A forming die provides the geometry and mechanical constraints required to transform the blank into the designed component.
The working surfaces of the die determine where the material can move and where deformation takes place.
A typical forming system may include:
- Punch
- Die surface
- Pressure pad or blank holder
- Guide system
- Forming inserts
- Supporting structures
The exact configuration depends on the product geometry and manufacturing requirements.
The forming die must maintain sufficient strength and rigidity while controlling the material throughout the press stroke.
For complex automotive components, even a small change in a forming surface or transition radius can affect material flow and final dimensional accuracy.
Why Material Flow Matters
Material flow is particularly important when forming automotive components with deep shapes, curved surfaces, ribs, or multiple transitions.
If the material cannot flow sufficiently into the required area, excessive tensile strain may develop. This can result in thinning or cracking.
On the other hand, if too much material accumulates in an area, compressive instability may occur and create wrinkles.
Therefore, successful forming requires a controlled balance between material movement and deformation.
Engineers may analyze material flow during the tooling development stage to identify potential forming problems before the die enters manufacturing.
Elastic and Plastic Deformation
Another important part of the metal forming principle is the difference between elastic and plastic deformation.
Elastic Deformation
Elastic deformation occurs when the material temporarily changes shape under load and returns toward its original condition after the force is removed.
This behavior is important because it contributes to springback.
Plastic Deformation
Plastic deformation occurs when the applied stress exceeds the material’s yield strength.
The material undergoes permanent deformation and retains the new geometry after the forming load is released.
Industrial sheet metal forming relies primarily on controlled plastic deformation.
The objective is not simply to apply a large amount of force. The forming conditions must be controlled so that the material reaches the required geometry while remaining within acceptable forming limits.
What Is Springback?
After the forming load is released, the sheet may partially return toward its original shape.
This phenomenon is called springback.
Springback is related to the elastic behavior remaining in the material after forming. It can affect:
- Part angles
- Curvature
- Flange position
- Dimensional accuracy
- Assembly performance
Springback can become more noticeable when forming high-strength steels because these materials generally have higher strength and different deformation characteristics compared with conventional mild steels.
For automotive stamping applications, engineers may compensate for expected springback through tooling geometry and process development.
Factors That Affect Metal Forming
The forming result is determined by several interacting variables rather than one single parameter.
Material Strength
Material strength affects the force required for deformation and the amount of forming that can be achieved before failure.
High-strength and advanced high-strength steels require particular attention to forming conditions because their strength and deformation behavior differ from conventional sheet materials.
Material Thickness
Sheet thickness influences forming force, stiffness, material flow, and dimensional stability.
A change in material thickness may therefore require adjustments to the forming strategy and tooling design.
Forming Radius
The radius of the punch and die affects local strain concentration.
A very small radius can increase local deformation and raise the risk of cracking, while an appropriately designed radius can provide a smoother transition for material flow.
Blank Holder Force
The blank holder or pressure system helps control how material enters the forming region.
Insufficient restraint may allow excessive material movement and create wrinkles, while excessive restraint can restrict material flow and increase tensile strain.
Lubrication
Friction between the sheet and forming surfaces affects material movement.
Proper lubrication can help control friction, improve material flow, reduce surface damage, and support stable production.
Tool Geometry
The geometry of the forming die determines the final shape of the component and strongly influences how strain is distributed throughout the sheet.
For complex automotive parts, transitions between flat surfaces, radii, walls, beads, and other features need to be carefully designed.
Metal Forming for Automotive Components
Automotive manufacturers use metal forming to produce many different types of components.
Examples include:
- Body panels
- Structural reinforcements
- Side members
- Brackets
- Cross members
- Pillar components
- Floor components
- Battery-related structural parts
The required forming strategy depends on the geometry, material, thickness, production volume, and dimensional requirements of each component.
Large automotive body components often require careful control of material flow because their surfaces can contain significant curvature and complex transitions.
Smaller structural components may require a combination of bending, forming, and local deformation to achieve the required stiffness and assembly geometry.
How Engineers Control the Forming Process
A successful forming process begins before the physical die is manufactured.
Engineers normally evaluate the product geometry and material requirements first. The forming direction, blank shape, forming depth, radii, material flow, and press requirements are then considered during process development.
Modern tooling development may include:
- Product geometry analysis
- Material and thickness evaluation
- Forming process planning
- Forming simulation
- Tool surface development
- Die manufacturing
- Die assembly
- Tryout and adjustment
- Dimensional inspection
- Production validation
The objective is to develop a forming process that can repeatedly produce the required geometry under stable production conditions.
Metal Forming and High-Strength Steel
The increasing use of high-strength steel has made forming control even more important in automotive manufacturing.
High-strength materials can help reduce vehicle weight while maintaining structural performance, but their forming behavior must be carefully considered during tooling development.
Potential issues include:
- Increased springback
- Localized strain
- Cracking
- Dimensional deviation
- Tool loading
- Material flow difficulties
For this reason, the forming principle must be considered together with material properties rather than treating the die geometry as an isolated factor.
Why Forming Principle Matters in Stamping Die Design
A stamping die is not simply a tool that forces metal into a shape.
Its working surfaces, pressure systems, radii, clearances, and material-control features must work together to manage deformation.
A successful forming die should provide:
- Controlled material flow
- Stable deformation
- Appropriate forming forces
- Consistent part geometry
- Reduced risk of cracking and wrinkling
- Controlled springback
- Reliable production repeatability
This is why forming analysis is an important part of automotive tooling development.
Conclusion
The metal forming principle is based on controlled plastic deformation. A press transfers force through a forming die, while the tool geometry controls how the sheet metal bends, stretches, compresses, and flows.
The final result depends on the interaction between material properties, sheet thickness, forming radius, friction, pressure conditions, tool geometry, and process parameters.
For automotive stamping applications, understanding this principle helps engineers develop forming processes that achieve complex geometries while maintaining dimensional accuracy and production stability.
HONGXING specializes in the development and manufacturing of automotive stamping dies for sheet metal forming applications. By combining tooling engineering, precision machining, die tryout, and dimensional control, HONGXING supports the production of automotive structural components, body panels, brackets, reinforcements, and other formed sheet metal parts.
A well-designed forming process does more than create the desired shape. It controls how the material behaves throughout the operation, providing the foundation for consistent part quality and reliable automotive production.